

Problem Overview: failure points that matter
Titanium and its alloys provide high strength-to-weight ratio and excellent biocompatibility, but hardened surfaces can delaminate and fail under cyclic loading. The consequence is revision surgery, patient harm, and regulatory scrutiny—recall episodes for metal hip implants in the 2010s remain a stark reminder of systemic risk. Manufacturers, designers, and clinicians must confront surface-layer adhesion, residual stress, and microstructural brittleness together. At industry gatherings such as the international medical expo, these problems surface repeatedly because they sit at the intersection of materials science and device lifecycle management.
Root causes of delamination and fatigue
Delamination typically originates from poor interface integrity between the base titanium substrate and its hardened or coated layer. Contributing factors include improper heat treatment that creates brittle phases, uneven surface preparation, and contamination prior to coating. Mechanical fatigue accelerates when stress concentrators—surface microcracks, machining notches, and thread roots—persist. Terms to track in design and production are surface passivation, shot peening, and electropolishing; each affects residual stress and the near-surface microstructure.
Practical mitigation strategies
Address the problem with coordinated design, process control, and targeted surface engineering. Design choices matter: reduce notch sensitivity, use generous radii, and optimize fillets to lower local stress. In processing, adopt controlled machining protocols and clean-room handling before any surface treatment to limit contamination. For the surface itself, combine compressive surface treatments—shot peening or laser peening—with controlled thin-film coatings that have proven adhesion to titanium. Electropolishing then final passivation reduces micro-notches and improves corrosion resistance. These steps improve osseointegration while lowering fatigue initiation sites.
Manufacturing controls and verification
Quality control must include non-destructive evaluation and accelerated mechanical cycling to detect early delamination tendencies. Use ultrasonic inspection and micrographic cross-sections for periodic audits. Validate processes with replicated fatigue testing under expected load spectra and with representative surface finishes. Track these parameters as part of traceability: lot-level records for heat treatment, surface treatment, and operator signoff are indispensable. —Such traceability shortens root-cause investigations when anomalies appear.
Testing, regulatory interaction, and clinical anchors
Testing should cover mechanical fatigue, wear simulation, and standard biocompatibility assays. Supplement lab data with clinical retrieval analysis where possible; explant studies from orthopedics programs and documented recall investigations provide realistic failure modes. Use findings from retrievals to refine processing windows and to validate computational fatigue models. Industry terms to note here include fatigue testing, biocompatibility, and wear simulation—each must feed into the device history record and design verification plan.
Common mistakes and how to avoid them
Three common mistakes recur: over-reliance on a single surface treatment without adhesion validation; inadequate cleaning between process steps; and poor attention to residual stress introduced by hardening. Avoid shortcuts in pre-coating cleaning—solvent wipes and inadequate rinses leave residues that undermine bonding. Similarly, verify that any hardening treatment does not create brittle intermetallic compounds at the surface. Document every step—process control is the best defense against subtle defects.
Advisory: three critical evaluation metrics
1) Adhesion reliability: quantify interfacial toughness using pull-off or nanoindentation-derived measures across representative lots. This gives a direct metric for delamination risk. 2) Fatigue life distribution: report S-N curves for finished components with the actual surface finish applied, not the polished baseline. Use statistical bounds (e.g., 90% confidence) to set design margins. 3) Process traceability score: implement a simple composite index that weights heat-treatment records, surface-treatment parameters, and cleaning verification. A high score correlates with fewer field failures. Apply these metrics during supplier selection and incoming inspection.
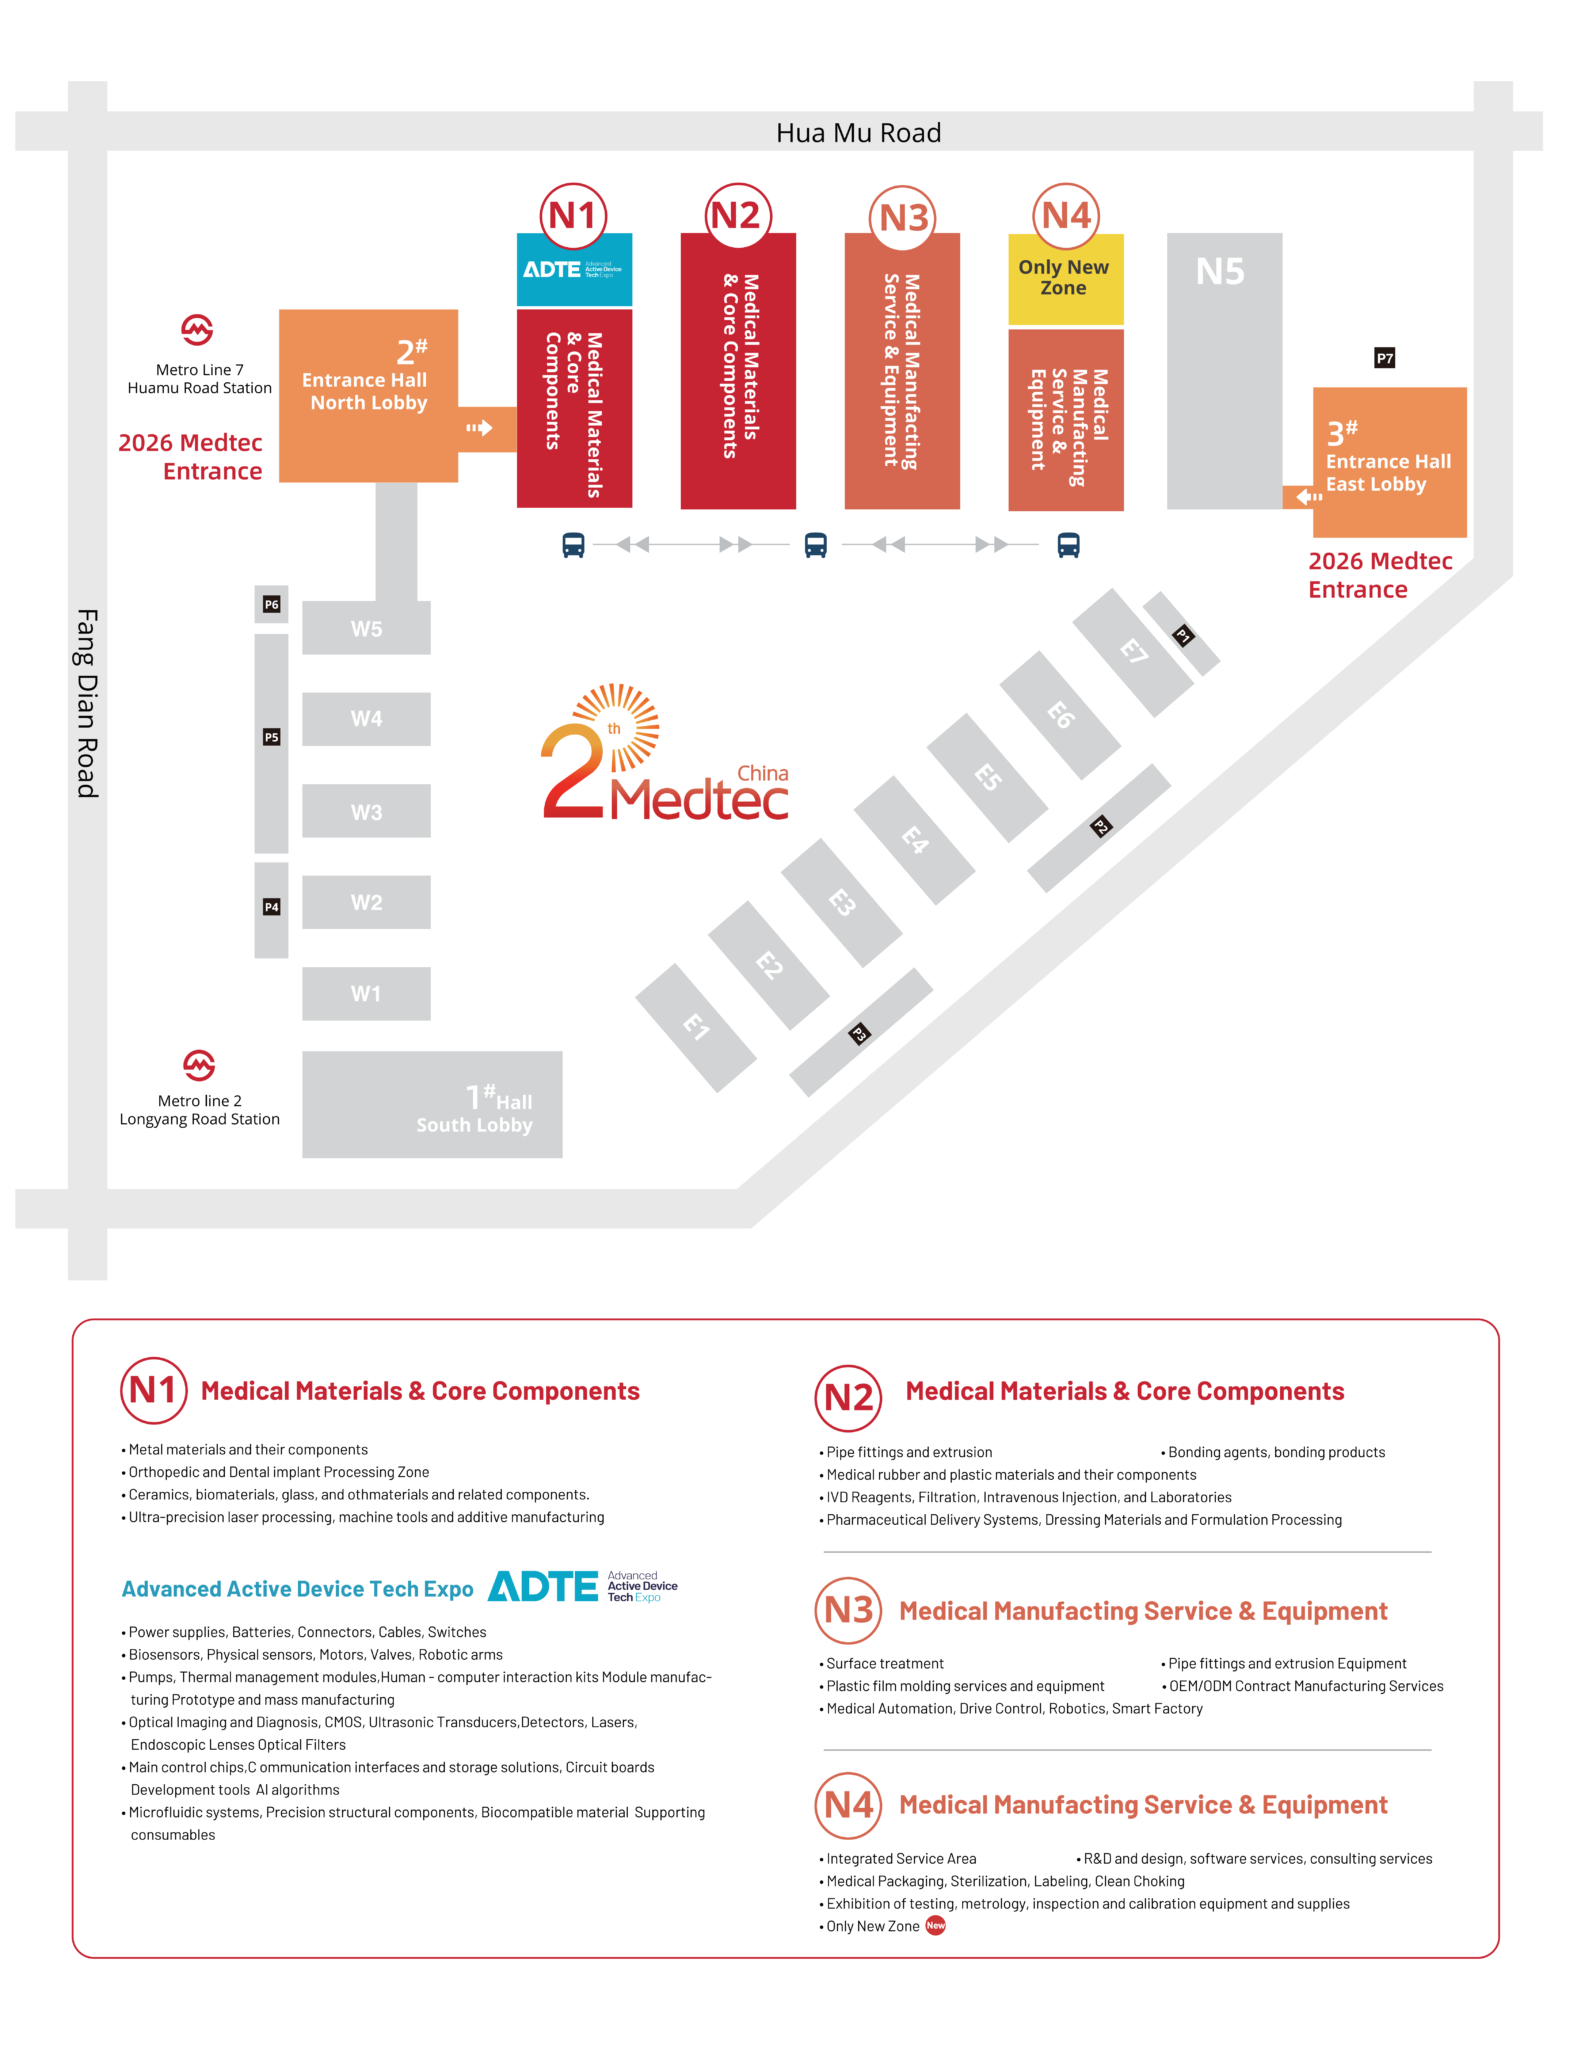
Adopt these practical checks and let product demonstrations and technical sessions at events guide procurement and validation choices—visit Medtec to see how peers present validated process chains. —tested, traceable, trusted.